- Products
- Air Compressors & Air Tools
- Climate Control
- Compaction Equipment
- Concrete Cutting Tools & Equipment
- Concrete and Masonry
- Demolition & Excavation
- Electrical & Mechanical
- Fasteners and Anchoring Adhesives
- Floor Protection
- Generators and Welders
- Hand Tools
- Heaters
- Janitorial and Office Supplies
- Jobsite Protection
- Ladders & Storage
- Lighting & Lighting Accessories
- Man Lifts
- Material Handling Equipment
- Power Tools
- Pressure Washers & Pumps
- Safety Gear
- Safety Products
- Saws
- Surface Preparation
- SEASONAL PRODUCTS
- Rentals
- Air Compressor and Air Tool Rentals
- Climate Control Rental
- Compaction Rentals
- Concrete Equipment Rentals
- Demolition & Excavation Equipment Rentals
- Concrete Floor Grinder Rentals
- General Construction Equipment Rentals
- Generator Rentals and Welder Rentals
- Heater Rentals
- Light Tower Rentals
- Man Lift Rentals in Massachusetts and Rhode Island
- Material Handling Equipment Rentals
- Pressure Washer & Pump Rentals
- Saw Rentals in New England
- SEASONAL PRODUCTS
- Products
- Air Compressors & Air Tools
- Climate Control
- Compaction Equipment
- Concrete Cutting Tools & Equipment
- Demolition & Excavation
- Electrical & Mechanical
- Floor Protection
- Generators and Welders
- Construction Heaters
- Construction Ladders, Staging, & Storage
- Construction Lighting
- Man Lifts
- Material Handling Equipment
- Industrial Janitorial and Office Supplies
- Pressure Washers & Pumps
- Construction Safety Products
- Construction Safety Gear
- Surface Preparation
- Building Protection
- Diesel Accessories
- Zero Emissions
- Rentals
- Air Compressor and Air Tool Rentals
- Climate Control Rental
- Compaction Rentals
- Concrete Equipment Rental
- Demolition & Excavation Equipment Rental
- General Construction Equipment Rental
- Generator Rentals and Welder Rentals
- Construction Heaters Rental
- Light Tower Rentals
- Man Lift Rentals
- Material Handling Equipment Rental
- Pressure Washer & Pump Rentals
- Saw Rentals in New England
- Concrete Floor Grinder Rentals
- Zero Emissions Rentals
- Repairs & Used
- Parts
- Blog
- Services
- Resources
- About Us
- Contact Us
Sales & Rental of Construction | Industrial Equipment & Supplies

China Top Velcro Abrasive Disc Manufacturers?
Finding reliable China Top Velcro Abrasive Disc Manufacturers requires more than comparing catalog prices. Buyers need evidence of abrasive consistency, hook-and-loop strength, backing quality, and production control. A disc may look identical in a product photo, yet perform differently on painted steel, hardwood, or automotive filler. Experienced purchasers usually request samples, grit specifications, coating details, and test results before approving a supplier.
This guide examines manufacturers through practical purchasing criteria. It considers factory experience, export capability, private-label support, quality systems, and communication reliability. Production details matter. A cleanly punched 125 mm disc should align smoothly with the sander, while its hook layer should remain attached during repeated use. Small defects can create vibration, uneven scratches, or wasted labor.
No ranking remains perfect. Supplier capacity changes.
Some companies excel at high-volume orders, while others serve smaller custom projects more carefully. Claims about durability should be checked against real application feedback, not accepted automatically. Buyers should also review material traceability, packaging protection, lead times, and after-sales handling. These factors often reveal more than a polished website.
For importers, distributors, and industrial users, selecting a dependable Velcro Abrasive Disc manufacturer involves balancing performance, cost, flexibility, and risk. The following overview offers a practical starting point for comparing leading Chinese suppliers. It also recognizes an uncomfortable point: the lowest quotation may become expensive when discs fail during production.
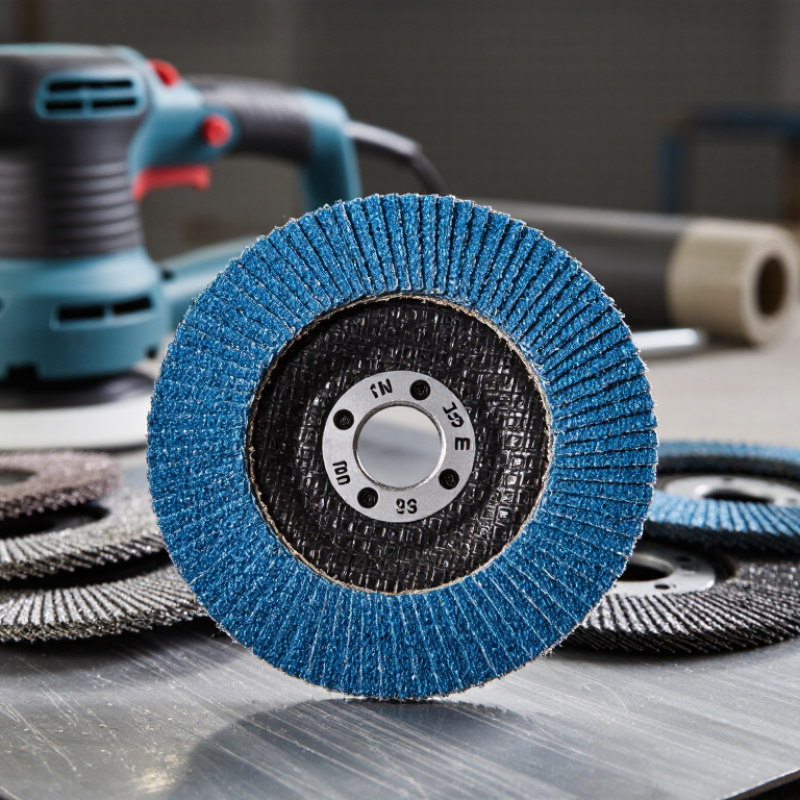
Table of Contents [Hide]
What Are Velcro Abrasive Discs and How Do They Work?
Velcro abrasive discs are coated sanding discs with a hook-and-loop backing. The disc attaches to a matching pad, much like a shoe fastener. Its abrasive grains cut paint, weld marks, wood fibers, or uneven metal surfaces. Operators can remove the disc within seconds. That matters in workshops where grit changes happen often.
The backing usually combines paper, cloth, or film with nylon hooks. The abrasive layer may contain aluminum oxide, silicon carbide, or ceramic grains. Grain shape controls cutting speed and surface finish. According to MarketsandMarkets’ Coated Abrasives Market report, this sector was valued at about USD 10.4 billion in 2023. It is projected to reach roughly USD 13.3 billion by 2028. Demand is linked to automotive repair, metalworking, and woodworking.
For buyers comparing Chinese manufacturers, technical proof matters more than catalogue photos. Check grit standards, disc diameter tolerance, hook density, adhesive bonding, and dust-hole alignment. FEPA and ANSI grading references help verify grit consistency. Grand View Research estimated the global abrasives market at more than USD 47 billion in 2023, showing the scale of this supply chain. Yet performance can vary between batches. In my workshop trials, a disc with strong initial cutting sometimes glazed too quickly on stainless steel. That result needs reflection. A lower-priced disc may save money, but uneven wear can increase labor and rework. Request batch samples, test them under identical pressure, and review quality records before placing large orders.
© Copyright - Pro Tool & Supply - Site by SVM E-Marketing Solutions - Sitemap
- Privacy policy