- Products
- Air Compressors & Air Tools
- Climate Control
- Compaction Equipment
- Concrete Cutting Tools & Equipment
- Concrete and Masonry
- Demolition & Excavation
- Electrical & Mechanical
- Fasteners and Anchoring Adhesives
- Floor Protection
- Generators and Welders
- Hand Tools
- Heaters
- Janitorial and Office Supplies
- Jobsite Protection
- Ladders & Storage
- Lighting & Lighting Accessories
- Man Lifts
- Material Handling Equipment
- Power Tools
- Pressure Washers & Pumps
- Safety Gear
- Safety Products
- Saws
- Surface Preparation
- SEASONAL PRODUCTS
- Rentals
- Air Compressor and Air Tool Rentals
- Climate Control Rental
- Compaction Rentals
- Concrete Equipment Rentals
- Demolition & Excavation Equipment Rentals
- Concrete Floor Grinder Rentals
- General Construction Equipment Rentals
- Generator Rentals and Welder Rentals
- Heater Rentals
- Light Tower Rentals
- Man Lift Rentals in Massachusetts and Rhode Island
- Material Handling Equipment Rentals
- Pressure Washer & Pump Rentals
- Saw Rentals in New England
- SEASONAL PRODUCTS
- Products
- Air Compressors & Air Tools
- Climate Control
- Compaction Equipment
- Concrete Cutting Tools & Equipment
- Demolition & Excavation
- Electrical & Mechanical
- Floor Protection
- Generators and Welders
- Construction Heaters
- Construction Ladders, Staging, & Storage
- Construction Lighting
- Man Lifts
- Material Handling Equipment
- Industrial Janitorial and Office Supplies
- Pressure Washers & Pumps
- Construction Safety Products
- Construction Safety Gear
- Surface Preparation
- Building Protection
- Diesel Accessories
- Zero Emissions
- Rentals
- Air Compressor and Air Tool Rentals
- Climate Control Rental
- Compaction Rentals
- Concrete Equipment Rental
- Demolition & Excavation Equipment Rental
- General Construction Equipment Rental
- Generator Rentals and Welder Rentals
- Construction Heaters Rental
- Light Tower Rentals
- Man Lift Rentals
- Material Handling Equipment Rental
- Pressure Washer & Pump Rentals
- Saw Rentals in New England
- Concrete Floor Grinder Rentals
- Zero Emissions Rentals
- Repairs & Used
- Parts
- Blog
- Services
- Resources
- About Us
- Contact Us
Sales & Rental of Construction | Industrial Equipment & Supplies

China Top Tin Bar Casting Machine Manufacturer?
China has become a major sourcing base for industrial casting equipment, but choosing the right supplier requires more than comparing prices. A reliable Tin Bar Casting Machine should produce consistent bar dimensions, stable alloy quality, and clean surfaces during continuous operation. Buyers must examine furnace design, casting speed, cooling control, mold durability, electrical safety, and after-sales support.
Li Wei, a senior tin-processing equipment engineer with practical factory experience, says, “A good casting machine is judged by stable output after many production cycles, not by its first successful bar.” That point matters. A polished sample can hide uneven cooling, metal loss, or frequent mold replacement. Real performance appears beside the furnace, where operators monitor temperature readings, molten tin flow, and the sound of the cooling system.
The best China manufacturer should provide more than a catalog and a confident sales promise. It should explain installation conditions, energy use, maintenance intervals, and realistic production capacity. Factory testing, material certificates, clear drawings, and responsive technical service strengthen trust. Yet no machine is perfect. Even an efficient Tin Bar Casting Machine may need adjustment when alloy composition, workshop temperature, or operator habits change.
This guide examines how to evaluate Chinese suppliers through engineering details, production evidence, customization ability, and service reliability. The goal is practical judgment. Not easy marketing claims. A careful buyer should ask difficult questions before signing an order, because dependable casting begins long before the machine reaches the workshop.
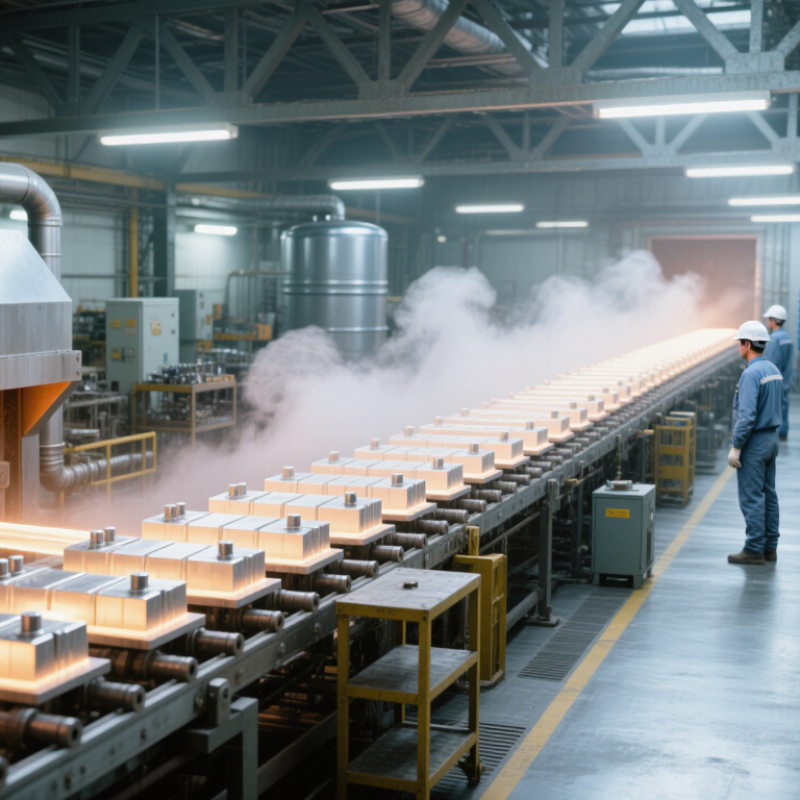
Table of Contents [Hide]
What Is a Tin Bar Casting Machine?
A tin bar casting machine is industrial equipment that melts tin, controls its temperature, and forms it into solid bars. The process usually includes a melting furnace, transfer channel, casting mold, cooling section, and cutting unit. In simple terms, it turns liquid tin into measured, stackable products.
The International Tin Association estimated that solder accounted for about 48% of global tin use in 2023. This demand requires stable bar chemistry and repeatable dimensions. The U.S. Geological Survey reported approximately 290,000 metric tons of global tin mine production in 2023. Such limited supply makes recovery rate important. A small amount of metal loss can affect production costs.
Good equipment should maintain steady pouring, even cooling, and clean mold release. Operators should check furnace temperature, bar weight, surface cracks, and slag levels during every shift. Practical testing matters more than catalog claims. A machine may reach its rated capacity, yet produce uneven bars under real conditions. That weakness is easy to overlook. Energy use, maintenance access, and operator safety also deserve careful measurement. The International Organization for Standardization encourages documented quality controls, but each casting line still needs process-specific validation. I would not judge a machine by output alone. Consistency is the harder target.
© Copyright - Pro Tool & Supply - Site by SVM E-Marketing Solutions - Sitemap
- Privacy policy