- Products
- Air Compressors & Air Tools
- Climate Control
- Compaction Equipment
- Concrete Cutting Tools & Equipment
- Concrete and Masonry
- Demolition & Excavation
- Electrical & Mechanical
- Fasteners and Anchoring Adhesives
- Floor Protection
- Generators and Welders
- Hand Tools
- Heaters
- Janitorial and Office Supplies
- Jobsite Protection
- Ladders & Storage
- Lighting & Lighting Accessories
- Man Lifts
- Material Handling Equipment
- Power Tools
- Pressure Washers & Pumps
- Safety Gear
- Safety Products
- Saws
- Surface Preparation
- SEASONAL PRODUCTS
- Rentals
- Air Compressor and Air Tool Rentals
- Climate Control Rental
- Compaction Rentals
- Concrete Equipment Rentals
- Demolition & Excavation Equipment Rentals
- Concrete Floor Grinder Rentals
- General Construction Equipment Rentals
- Generator Rentals and Welder Rentals
- Heater Rentals
- Light Tower Rentals
- Man Lift Rentals in Massachusetts and Rhode Island
- Material Handling Equipment Rentals
- Pressure Washer & Pump Rentals
- Saw Rentals in New England
- SEASONAL PRODUCTS
- Products
- Air Compressors & Air Tools
- Climate Control
- Compaction Equipment
- Concrete Cutting Tools & Equipment
- Demolition & Excavation
- Electrical & Mechanical
- Floor Protection
- Generators and Welders
- Construction Heaters
- Construction Ladders, Staging, & Storage
- Construction Lighting
- Man Lifts
- Material Handling Equipment
- Industrial Janitorial and Office Supplies
- Pressure Washers & Pumps
- Construction Safety Products
- Construction Safety Gear
- Surface Preparation
- Building Protection
- Diesel Accessories
- Zero Emissions
- Rentals
- Air Compressor and Air Tool Rentals
- Climate Control Rental
- Compaction Rentals
- Concrete Equipment Rental
- Demolition & Excavation Equipment Rental
- General Construction Equipment Rental
- Generator Rentals and Welder Rentals
- Construction Heaters Rental
- Light Tower Rentals
- Man Lift Rentals
- Material Handling Equipment Rental
- Pressure Washer & Pump Rentals
- Saw Rentals in New England
- Concrete Floor Grinder Rentals
- Zero Emissions Rentals
- Repairs & Used
- Parts
- Blog
- Services
- Resources
- About Us
- Contact Us
Sales & Rental of Construction | Industrial Equipment & Supplies

What Are the Best Shower Glass Manufacturers in China?
Choosing the best Shower Glass manufacturer in China requires more than comparing prices. The right supplier must combine safe materials, precise processing, dependable hardware, and consistent production control. A polished showroom sample can look impressive. The real test appears in the factory, packaging area, and after-sales records.
Li Wei, a China-based shower enclosure quality consultant, says, “Reliable glass is judged by its process, not its shine.” This practical view matters. Buyers should examine tempered glass thickness, edge finishing, hole accuracy, and visible distortion. They should also request test reports, factory photographs, and clear explanations of quality inspections. Compliance documentation deserves careful review.
Details reveal experience.
Leading manufacturers usually offer stable glass specifications, custom sizes, and tested fittings for different bathroom environments. Their teams should understand moisture exposure, installation tolerances, and transport risks. Strong suppliers can explain how they prevent scratches, corner damage, and hardware corrosion during shipment. They should also provide realistic lead times, sample approval procedures, and replacement policies.
Still, no supplier is perfect. A factory may have modern equipment but weak communication. Another may offer excellent prices but limited customization. This is where buyers need patience and independent verification. Visiting the facility, checking recent export experience, and speaking with existing customers can expose gaps that brochures hide. The best Shower Glass manufacturer is not simply the cheapest option. It is the partner that delivers safe, attractive, consistent products after the order leaves the sales office.
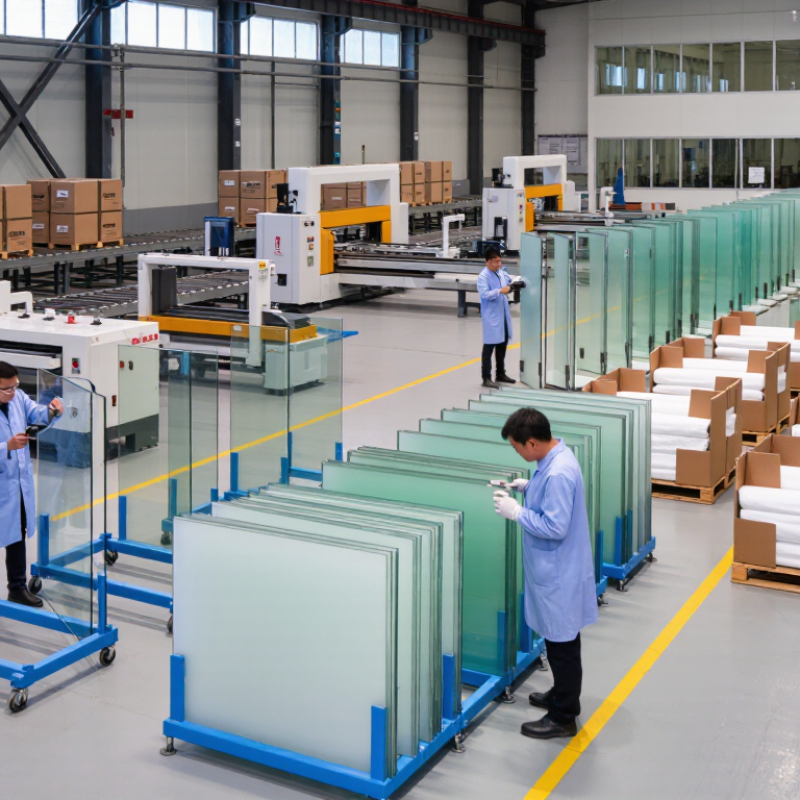
Table of Contents [Hide]
What Makes a Shower Glass Manufacturer in China Reliable?
What Makes a Shower Glass Manufacturer in China Reliable?
A reliable shower glass manufacturer in China shows more than polished product photos. Its factory should explain glass thickness, tempering methods, edge polishing, and hardware compatibility clearly. Experienced manufacturers usually maintain stable production records and traceable inspection reports. They can provide samples before mass production, allowing buyers to check clarity, flatness, drilling accuracy, and surface quality. Ask about relevant safety standards and independent testing. Vague answers deserve attention.
Tips: Request a factory video call, not only catalog images. Check production lines, storage areas, and packing methods. Compare a sample with its approved specification. Confirm lead times, replacement procedures, and communication responsibilities in writing. Small details often reveal large differences.
Reliable suppliers also control moisture protection during export packing. Each glass panel should have clear labels and impact-resistant separation. Quality teams should inspect scratches, chips, dimensions, and tempering results before shipment. A professional manufacturer will discuss possible defects honestly instead of promising perfection. That matters. No production process is flawless, and pretending otherwise weakens trust. In my view, the strongest supplier is not always the cheapest one. It is the company that explains risks, keeps records, responds quickly, and corrects mistakes with evidence. A site audit or third-party inspection can strengthen this judgment, although it cannot replace careful communication throughout the project.
© Copyright - Pro Tool & Supply - Site by SVM E-Marketing Solutions - Sitemap
- Privacy policy