- Products
- Air Compressors & Air Tools
- Climate Control
- Compaction Equipment
- Concrete Cutting Tools & Equipment
- Concrete and Masonry
- Demolition & Excavation
- Electrical & Mechanical
- Fasteners and Anchoring Adhesives
- Floor Protection
- Generators and Welders
- Hand Tools
- Heaters
- Janitorial and Office Supplies
- Jobsite Protection
- Ladders & Storage
- Lighting & Lighting Accessories
- Man Lifts
- Material Handling Equipment
- Power Tools
- Pressure Washers & Pumps
- Safety Gear
- Safety Products
- Saws
- Surface Preparation
- SEASONAL PRODUCTS
- Rentals
- Air Compressor and Air Tool Rentals
- Climate Control Rental
- Compaction Rentals
- Concrete Equipment Rentals
- Demolition & Excavation Equipment Rentals
- Concrete Floor Grinder Rentals
- General Construction Equipment Rentals
- Generator Rentals and Welder Rentals
- Heater Rentals
- Light Tower Rentals
- Man Lift Rentals in Massachusetts and Rhode Island
- Material Handling Equipment Rentals
- Pressure Washer & Pump Rentals
- Saw Rentals in New England
- SEASONAL PRODUCTS
- Products
- Air Compressors & Air Tools
- Climate Control
- Compaction Equipment
- Concrete Cutting Tools & Equipment
- Demolition & Excavation
- Electrical & Mechanical
- Floor Protection
- Generators and Welders
- Construction Heaters
- Construction Ladders, Staging, & Storage
- Construction Lighting
- Man Lifts
- Material Handling Equipment
- Industrial Janitorial and Office Supplies
- Pressure Washers & Pumps
- Construction Safety Products
- Construction Safety Gear
- Surface Preparation
- Building Protection
- Diesel Accessories
- Zero Emissions
- Rentals
- Air Compressor and Air Tool Rentals
- Climate Control Rental
- Compaction Rentals
- Concrete Equipment Rental
- Demolition & Excavation Equipment Rental
- General Construction Equipment Rental
- Generator Rentals and Welder Rentals
- Construction Heaters Rental
- Light Tower Rentals
- Man Lift Rentals
- Material Handling Equipment Rental
- Pressure Washer & Pump Rentals
- Saw Rentals in New England
- Concrete Floor Grinder Rentals
- Zero Emissions Rentals
- Repairs & Used
- Parts
- Blog
- Services
- Resources
- About Us
- Contact Us
Sales & Rental of Construction | Industrial Equipment & Supplies

2026 Best Cylindrical Cell Assembly Machines?
Choosing the 2026 Best Cylindrical Cell Assembly Machines requires more than comparing catalog speed.
A reliable assessment examines the complete production path, from electrode handling to final electrical testing. Cylindrical Cell Assembly Machines must maintain accurate jelly-roll alignment, stable tab welding, controlled electrolyte filling, and consistent crimping. Small errors can create visible defects, leakage risks, or unstable capacity results. The best equipment connects these stages without hiding process weaknesses.
Real factory conditions matter.
This guide evaluates machines through practical indicators, including throughput, yield, changeover time, automation depth, and maintenance access. It also considers whether operators can trace each cell through barcode records, camera inspections, pressure checks, and formation data. A fast line means little if it produces excessive rejects or requires frequent manual correction. Energy consumption, floor space, spare-part availability, and supplier response times deserve equal attention.
Technical brochures are not enough.
Factory acceptance testing, sample production, and verified performance data should support every serious purchasing decision. Engineers should compare results using the same cell format, materials, and operating conditions. Even experienced teams can overlook integration delays between welding, filling, sealing, and testing modules. That weakness deserves honest attention.
No ranking is perfect.
This introduction frames a careful comparison of leading 2026 solutions, while recognizing that the right machine depends on cell design, production volume, quality targets, and budget. Readers will find practical criteria rather than impressive claims alone. The goal is dependable manufacturing, measurable quality, and a clearer path from pilot production to stable commercial output.
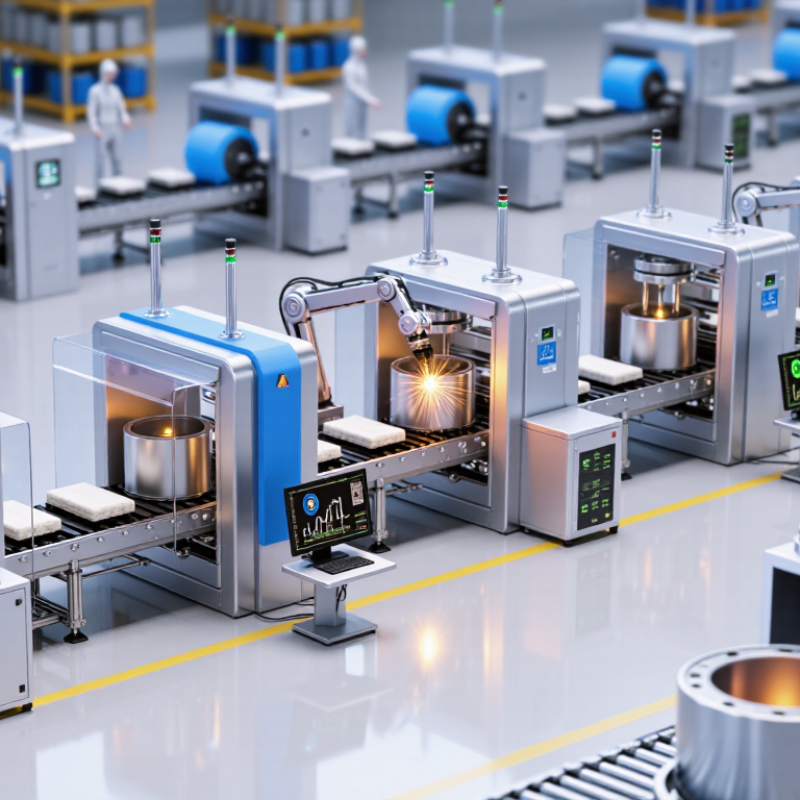
Table of Contents [Hide]
Cylindrical Cell Assembly Machines: Definition and Core Functions
Cylindrical cell assembly machines are integrated production systems for building rechargeable cells from prepared electrodes, separators, collectors, and metal cans. They manage delicate steps with controlled pressure, speed, temperature, and alignment. In practical production, even a small electrode offset can affect internal resistance and safety. Precision matters.
Core functions usually include electrode winding, separator placement, jelly-roll insertion, tab forming, welding, electrolyte filling, crimping, and final sealing.
Some systems also perform vacuum handling, leak testing, insulation checks, weighing, and electrical inspection. Sensors record critical data, such as weld energy, filling weight, and sealing force. This traceability helps engineers investigate defects instead of guessing.
When comparing the best cylindrical cell assembly machines for 2026, manufacturers should examine format flexibility, changeover time, line stability, and inspection depth. A fast machine is not always the best machine. Poor alignment can create expensive rework. Automation reduces manual variation, but it does not remove the need for trained operators. No machine is perfect. Maintenance access, spare-part availability, and process validation deserve equal attention. In my view, suppliers should test representative materials before purchase, because laboratory results can differ from continuous production. A machine may meet its advertised cycle time, yet still struggle with dust control, thin separators, or unstable welding conditions.
© Copyright - Pro Tool & Supply - Site by SVM E-Marketing Solutions - Sitemap
- Privacy policy