- Products
- Air Compressors & Air Tools
- Climate Control
- Compaction Equipment
- Concrete Cutting Tools & Equipment
- Concrete and Masonry
- Demolition & Excavation
- Electrical & Mechanical
- Fasteners and Anchoring Adhesives
- Floor Protection
- Generators and Welders
- Hand Tools
- Heaters
- Janitorial and Office Supplies
- Jobsite Protection
- Ladders & Storage
- Lighting & Lighting Accessories
- Man Lifts
- Material Handling Equipment
- Power Tools
- Pressure Washers & Pumps
- Safety Gear
- Safety Products
- Saws
- Surface Preparation
- SEASONAL PRODUCTS
- Rentals
- Air Compressor and Air Tool Rentals
- Climate Control Rental
- Compaction Rentals
- Concrete Equipment Rentals
- Demolition & Excavation Equipment Rentals
- Concrete Floor Grinder Rentals
- General Construction Equipment Rentals
- Generator Rentals and Welder Rentals
- Heater Rentals
- Light Tower Rentals
- Man Lift Rentals in Massachusetts and Rhode Island
- Material Handling Equipment Rentals
- Pressure Washer & Pump Rentals
- Saw Rentals in New England
- SEASONAL PRODUCTS
- Products
- Air Compressors & Air Tools
- Climate Control
- Compaction Equipment
- Concrete Cutting Tools & Equipment
- Demolition & Excavation
- Electrical & Mechanical
- Floor Protection
- Generators and Welders
- Construction Heaters
- Construction Ladders, Staging, & Storage
- Construction Lighting
- Man Lifts
- Material Handling Equipment
- Industrial Janitorial and Office Supplies
- Pressure Washers & Pumps
- Construction Safety Products
- Construction Safety Gear
- Surface Preparation
- Building Protection
- Diesel Accessories
- Zero Emissions
- Rentals
- Air Compressor and Air Tool Rentals
- Climate Control Rental
- Compaction Rentals
- Concrete Equipment Rental
- Demolition & Excavation Equipment Rental
- General Construction Equipment Rental
- Generator Rentals and Welder Rentals
- Construction Heaters Rental
- Light Tower Rentals
- Man Lift Rentals
- Material Handling Equipment Rental
- Pressure Washer & Pump Rentals
- Saw Rentals in New England
- Concrete Floor Grinder Rentals
- Zero Emissions Rentals
- Repairs & Used
- Parts
- Blog
- Services
- Resources
- About Us
- Contact Us
Sales & Rental of Construction | Industrial Equipment & Supplies

2026 Best China Leading Square Bottom FIBC Supplier?
In 2026, buyers are asking a practical question: which China Leading Square Bottom Fibc Supplier can deliver stable quality, not merely attractive quotations? Square-bottom FIBCs support upright stacking, cleaner warehouse handling, and more predictable pallet utilization. These details matter when each filled bag contains hundreds or thousands of kilograms.
Market evidence supports continued demand. Grand View Research estimated the global FIBC market at approximately USD 5.37 billion in 2022 and projected a 6.3% compound annual growth rate through 2030. IMARC Group reported a global market value of about USD 6.1 billion in 2023, with further expansion expected during 2024–2032. Estimates vary. That difference deserves attention, because research methods and market definitions are not identical.
A credible supplier should explain its fabric denier, coating weight, safe working load, safety factor, stitching design, and discharge configuration. It should also provide batch records, inspection reports, and traceable raw-material information. ISO 21898 offers a useful reference for flexible intermediate bulk container performance and handling requirements. Third-party testing remains valuable for demanding applications, including minerals, chemicals, food ingredients, and construction materials. Experience matters here. A reliable factory can show how it controls seam strength, moisture protection, dimensions, and printing consistency on the production floor.
No supplier is perfect. A polished website is not evidence. Buyers should review samples, factory capabilities, corrective-action records, and delivery history before signing a contract. This guide evaluates leading Chinese manufacturers through measurable criteria, practical risk checks, and the realities of international procurement. Performance should come before promises.
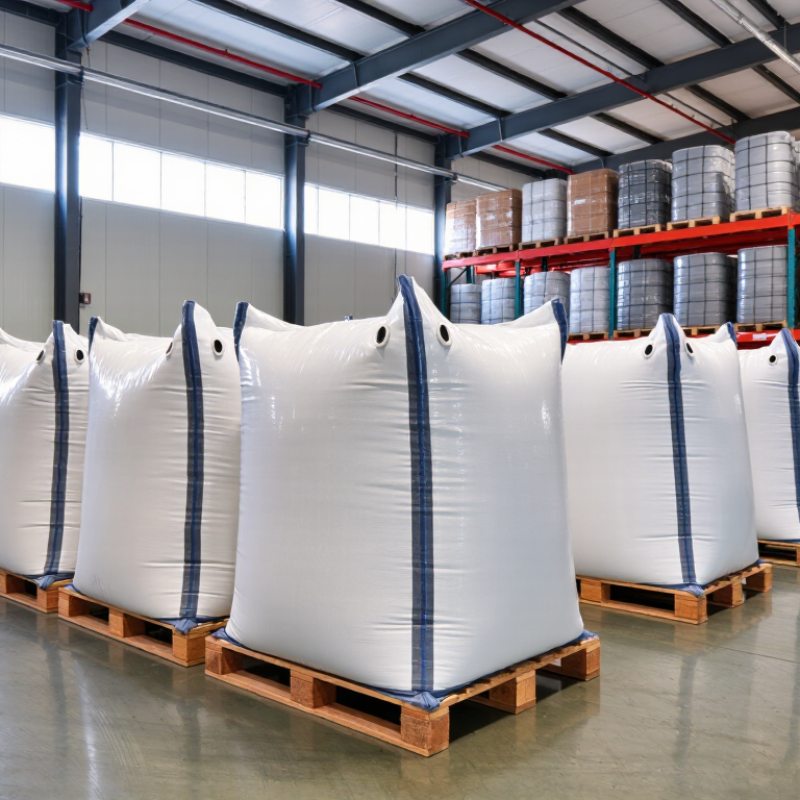
Table of Contents [Hide]
What Is a Square Bottom FIBC and How Does It Work?
2026 Best China Leading Square Bottom FIBC Supplier?
What Is a Square Bottom FIBC and How Does It Work?
A square bottom FIBC is a flexible bulk bag designed with a flat, stable base. Unlike a rounded bag, it stands more evenly on pallets, warehouse floors, and truck beds. Its body usually uses woven polypropylene fabric with four vertical panels. Filling typically happens through a top spout, while discharge uses a bottom spout or flat-bottom opening.
The square shape improves space use. Bags can sit closer together with fewer gaps. Grand View Research’s FIBC market analysis identifies food, chemicals, agriculture, and construction as major demand sectors. The same analysis reports continued market growth, supported by reusable bulk packaging and efficient transport.
Typical FIBCs carry about 500 to 2,000 kilograms, depending on fabric strength, seam design, and safety factor.
Performance depends on details. ISO 21898 requires testing for design, lifting, stacking, and safe working load. A reliable Chinese supplier should provide test records, production traceability, fabric specifications, and lifting-loop inspections. The bag must also match the material’s flow behavior.
Fine powder may need a coated fabric or special liner. Moist products create another problem. A square base is helpful, but it is not magic. Poor filling, uneven loading, or weak seams can still cause tilting.
In my experience, prototype loading tests reveal problems that drawings often miss.
© Copyright - Pro Tool & Supply - Site by SVM E-Marketing Solutions - Sitemap
- Privacy policy